
Key Facts
- 54,000 lb/hr EG solution feed
- 30,000 lb/hr Water removal
- 90 wt.% EG bottoms concentration
- <30 ppm EG in overhead vapor
Long-Term Ethylene Glycol Recovery Through Dualflo® Distillation Technology
Executive Summary
Pratt & Whitney implemented a custom ethylene glycol distillation system designed by Artisan Industries, incorporating proprietary Dualflo® distillation trays to efficiently separate water from ethylene glycol while minimizing fouling, product losses, and maintenance-related downtime.
The system delivered reliable separation performance and long-term operational benefits, including:
- Processing of 54,000 lb/hr (108 gpm) of ethylene glycol solution containing 40% EG
- Removal of 30,000 lb/hr (60 gpm) of water from the incoming solution
- Concentration of ethylene glycol to 90% by weight in the column bottoms
- Achievement of less than 30 ppm EG in the overhead water vapor
- No downtime attributed to Dualflo® trays, with continuous operation reported since installation in 1999
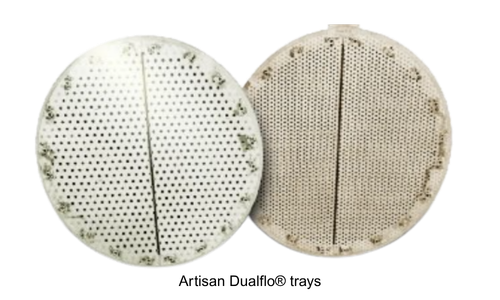
- Reduced fouling potential through a simplified tray design capable of handling sediment-containing streams
This project demonstrates how Artisan’s Dualflo® distillation technology can deliver high-performance separation, fouling resistance, and long-term operational reliability in demanding industrial applications.
Background
Pratt & Whitney required a reliable distillation system to concentrate an ethylene glycol solution containing 40% EG, water, and sediment. The presence of solids created potential fouling and maintenance challenges for conventional distillation equipment.
Building on a previous installation in 1966, Artisan
designed a new system featuring its proprietary Dualflo® trays, which use a simplified design without downcomers to minimize fouling. The system incorporated a thermosiphon reboiler, an internal overhead condenser, and feed preheating to support efficient separation, energy conservation, and long-term operational reliability.
The Challenge
The existing recovery system was constrained by both technical and economic factors:
- Fouling in distillation columns caused by tarry residues and solids
- Frequent cleaning shutdowns, limiting effective operating time
- Recovery capacity bottlenecks, preventing utilization of available solvent streams
- High disposal costs, averaging approximately $0.40 per gallon
- Lost solvent value, including both internal reuse and resale opportunities
In total, the site identified a multi-million-dollar annual opportunity tied directly to improving solvent recovery reliability and capacity.
The Solution
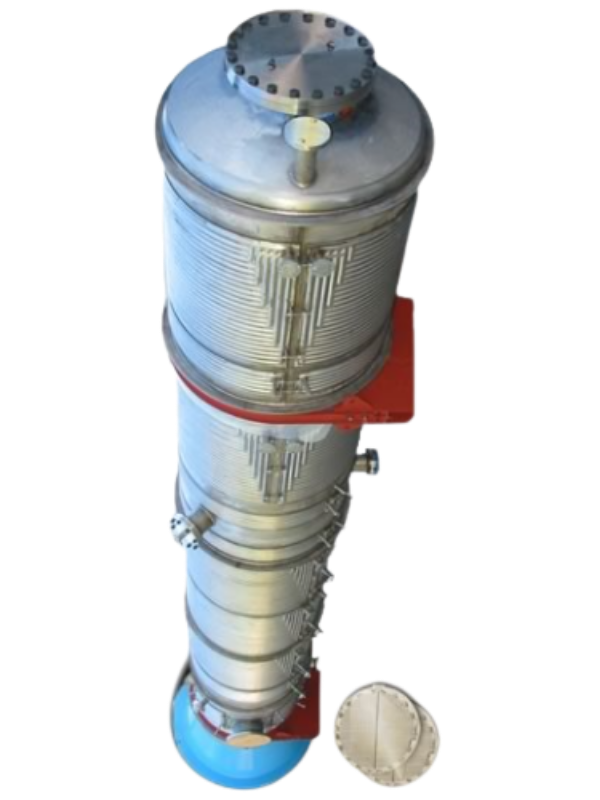
Artisan supplied a 9-foot-diameter distillation column approximately 55 feet tall, equipped with Dualflo® sieve trays without downcomers. The simple tray design helps the column stay clean when solids are present, with little to no fouling.
The final configuration included:
- Thermosiphon reboiler supplies the boil-up
- Internal overhead condenser provides reflux
- Feed is preheated with column bottoms to conserve energy
- Column design targets less than 30 ppm EG in overhead water vapor.
Equipment Profile
Following implementation, the solvent recovery system delivered measurable, site-level economic and operational gains.
WHY DUALFLO® MADE THE DIFFERENCE
- Dualflo® trays use a sieve-tray arrangement without downcomers. The case study attributes the absence of tray-related downtime to their simple design and ability to remain clean with solids present, limiting fouling.
BROADER APPLICABILITY
-
Artisan's Dualflo® distillation technology is well-suited for industrial applications requiring reliable liquid separation, minimal fouling, and continuous operation, particularly when processing streams containing solids or sediment.
Applications that may benefit include:
- Chemical Manufacturing: Concentration and purification of process liquids
- Solvent Recovery: Separation and recovery of valuable solvents for reuse
- Glycol Processing: Removal of water from ethylene glycol and similar solutions
- Specialty Chemicals: Distillation of process streams containing suspended solids or fouling materials
Conclusion
Artisan Industries’ Dualflo® distillation system demonstrates the value of innovative engineering, efficient separation, and long-term operational reliability in demanding industrial applications. By successfully concentrating ethylene glycol to 90% while maintaining less than 30 ppm EG in the overhead vapor, the system met Pratt & Whitney’s demanding process requirements. With continuous operation reported since 1999 and no downtime attributed to the Dualflo® trays, this project highlights Artisan’s ability to deliver durable, fouling-resistant separation solutions that support consistent performance and minimize maintenance challenges over time.
Download the Full Case Study PDF
Fill out the form below to receive an instant copy of this case study.